The Challenge: Rising Repair Bills, Poor Layout, and Production Risks
As a busy mid-sized workshop producing custom kitchen carcasses, Kitchen Generator generates 6 to 10 tonnes of wood waste per week, predominantly composed of MDF offcuts, chipboard, and fine dust. Disposing of this volume of waste off-site would incur prohibitive waste removal costs, making an on-site wood waste boiler essential for factory heating and waste management.
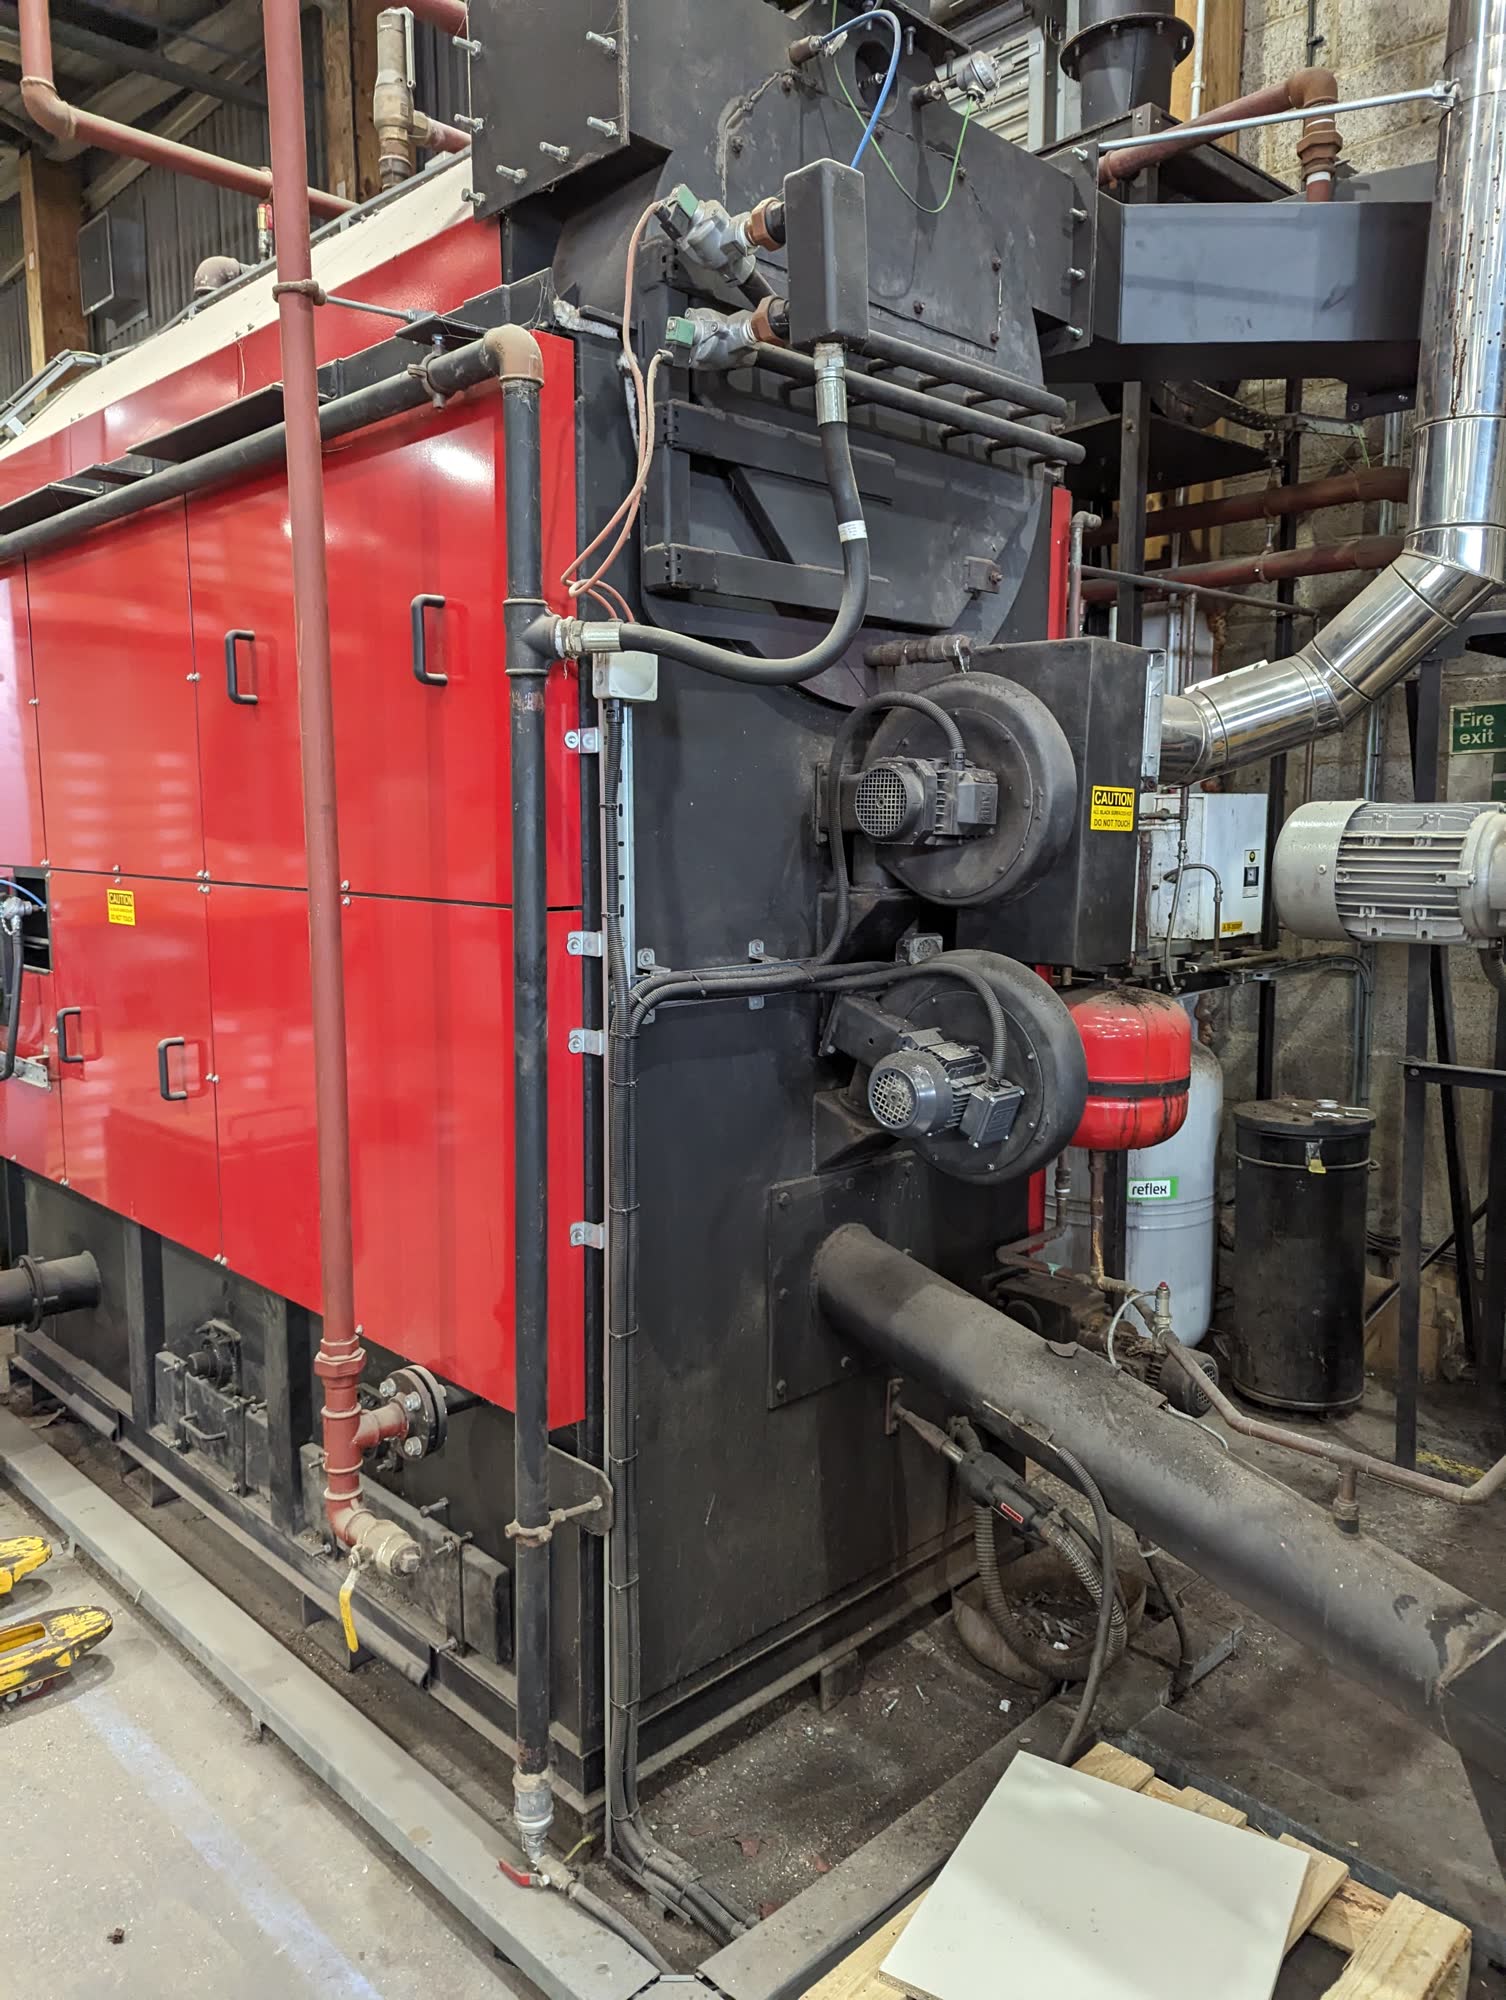
Kitchen Generator had a biomass boiler system purchased in 2018 from a competitor. However, over time this system created more problems than it solved and created an operational bottleneck:
- Escalating maintenance costs: The entire system needed more and more repairs as time went on, culminating in a £32,000 repair estimate from the original manufacturer.
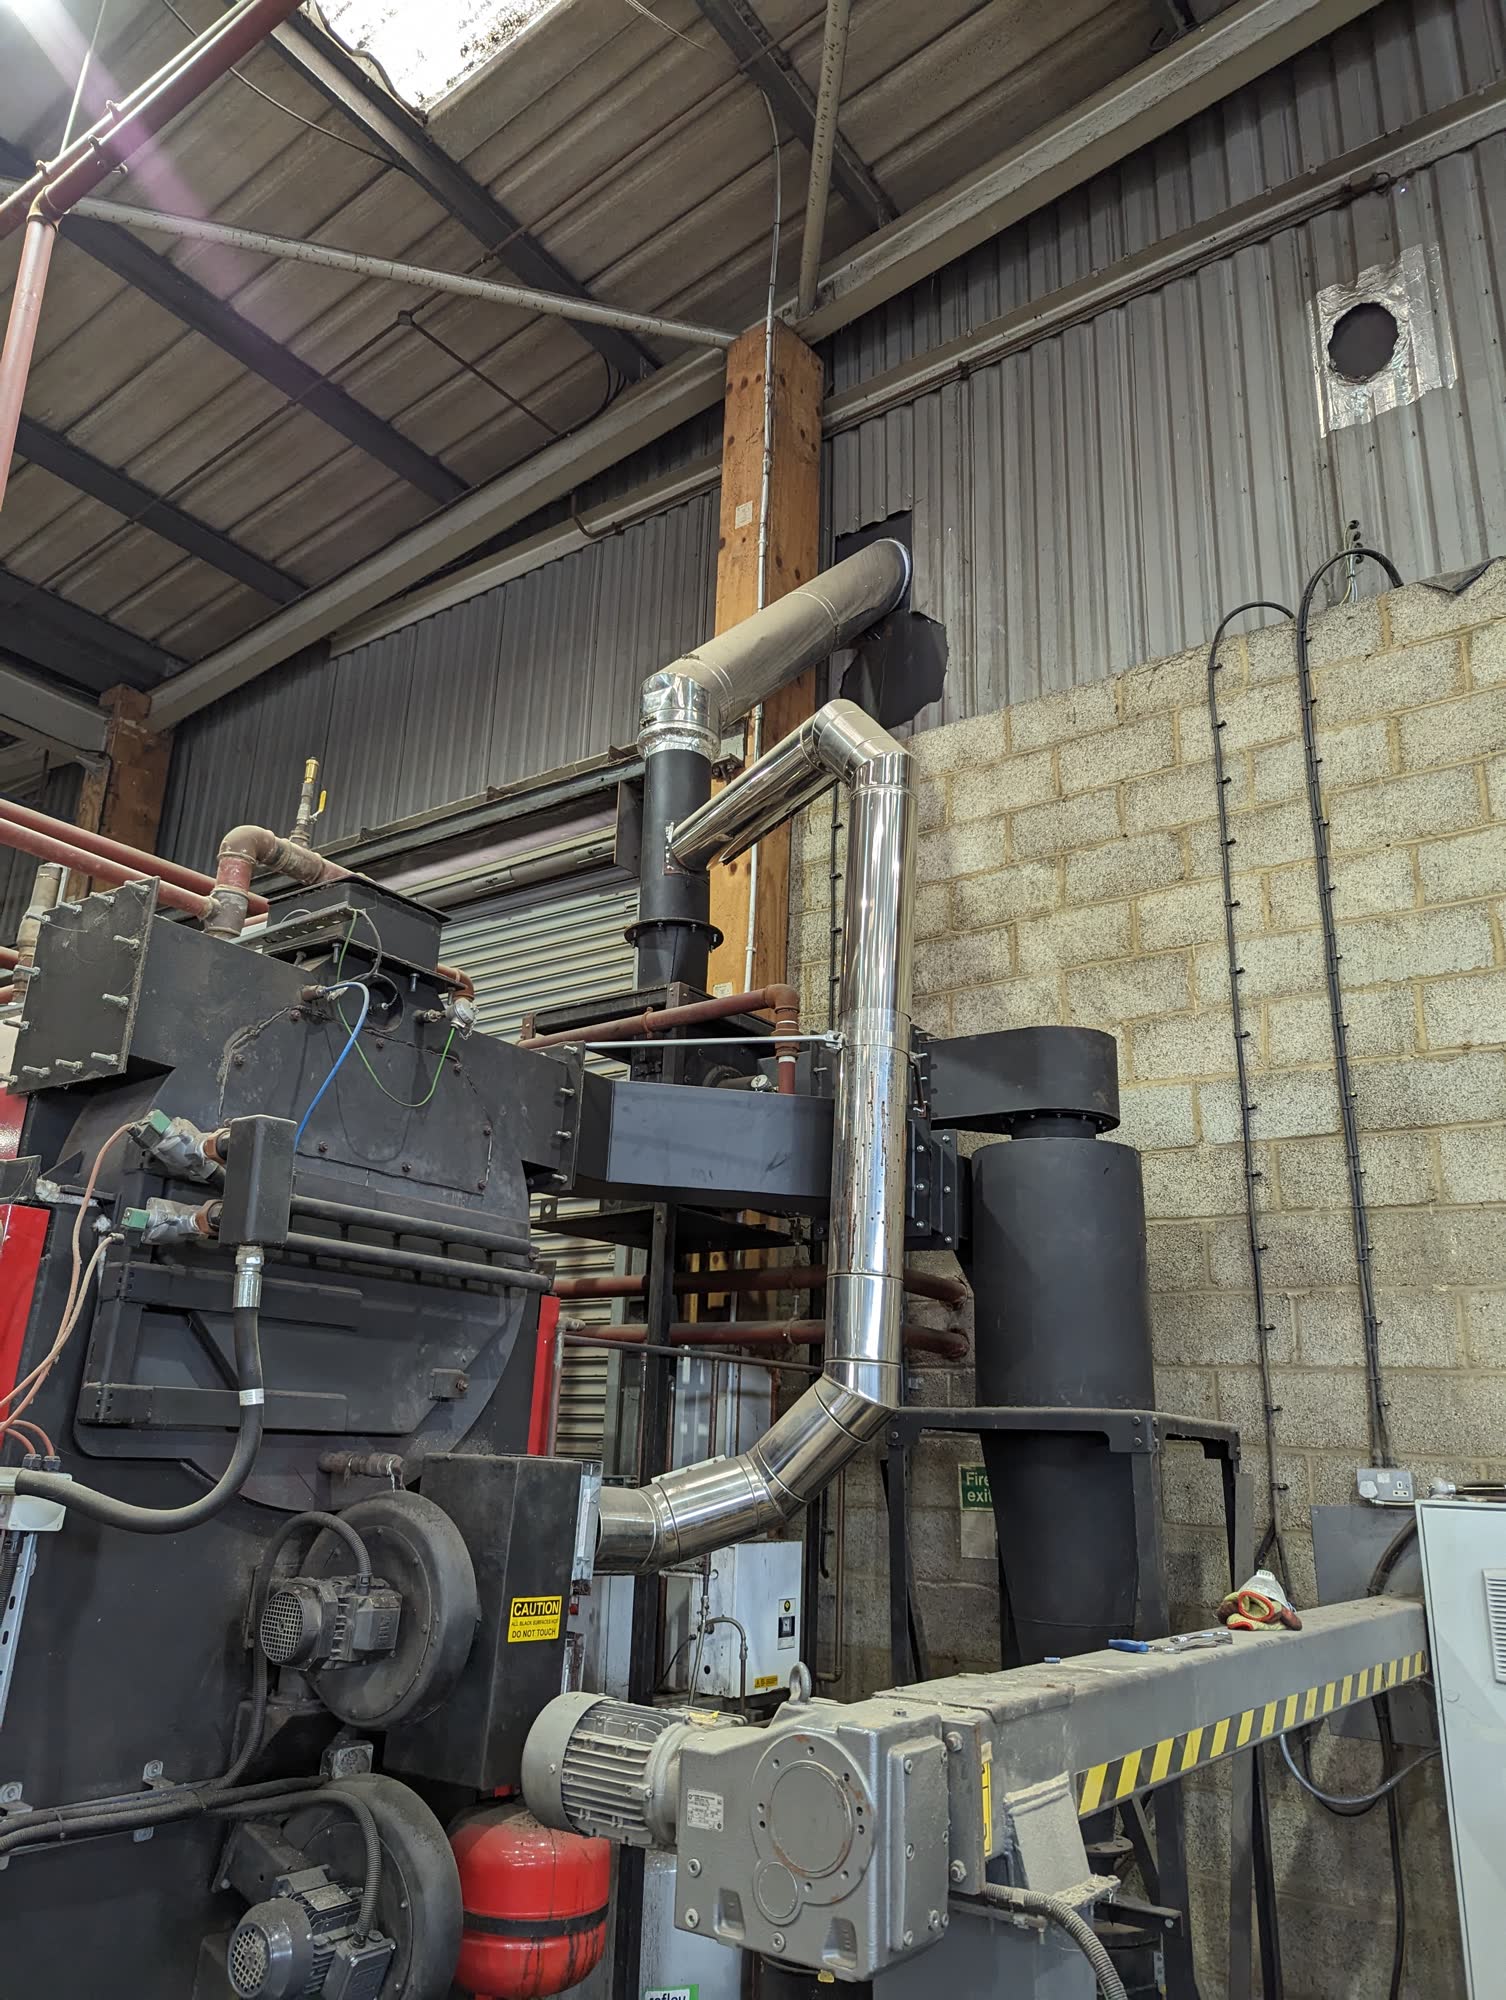
- Inaccessible Induced Draft (ID) fan placement: The competitor had installed the ID fan approximately three metres off the ground, meaning that any maintenance, cleaning, or inspection required hired equipment and unnecessary downtime. This was expensive and time-consuming, meaning that the placement of the ID fan created more problems than it solved.
- Silo overflow risks: With a large quantity of wood waste accumulating daily, any unplanned downtime threatened to fill or overflow the silo and essentially stall factory production entirely.
The team at Kitchen Generator were getting increasingly frustrated. They needed something straightforward and reliable that would not generate expensive repair bills. They also wanted to work with a company that would be more reliable on service and maintenance, something that we at Ranheat pride ourselves on.
The Solution: Install a Ranheat MSU300 and Improve the Layout of the System
Having first met Alexander at a trade show in 2024, Kitchen Generator got in touch with Ranheat in early 2026 after receiving the quote for £32,000 for repairs from the manufacturer. They asked us for a site visit and a quote for a new biomass heating system.
We were able to solve the problems caused by the system from the competitor.
Cost-Saving Integration with Existing Plant
We were able to reuse the existing silo, transfer screw, pipework, and dissipator, which saved money and time for all involved. We took away the old boiler in a part exchange.
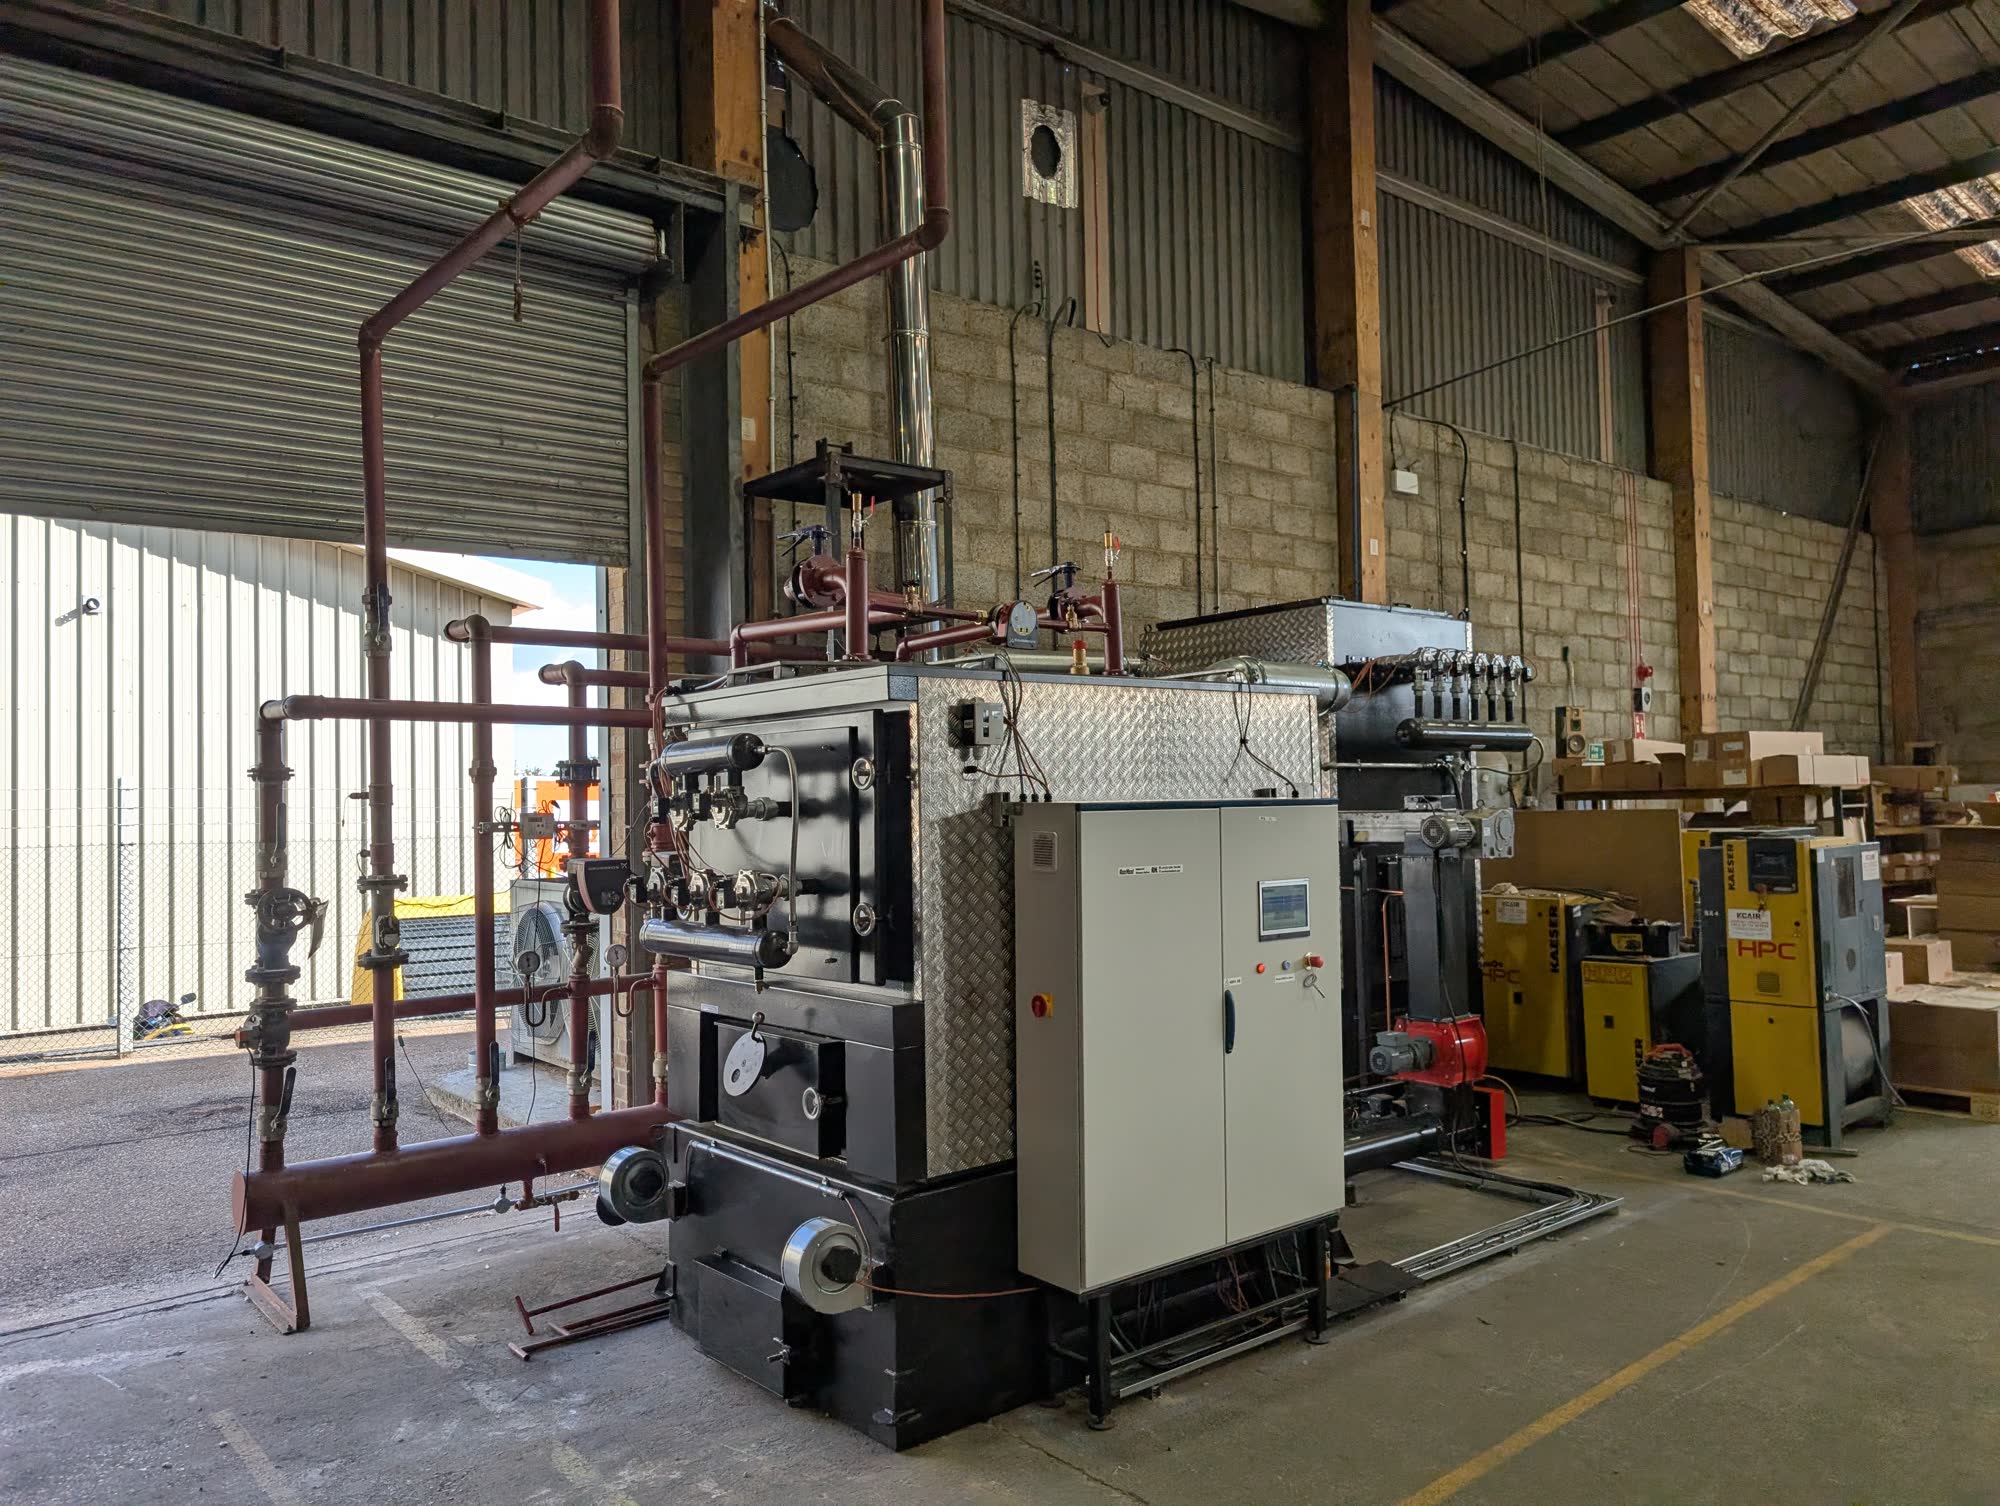
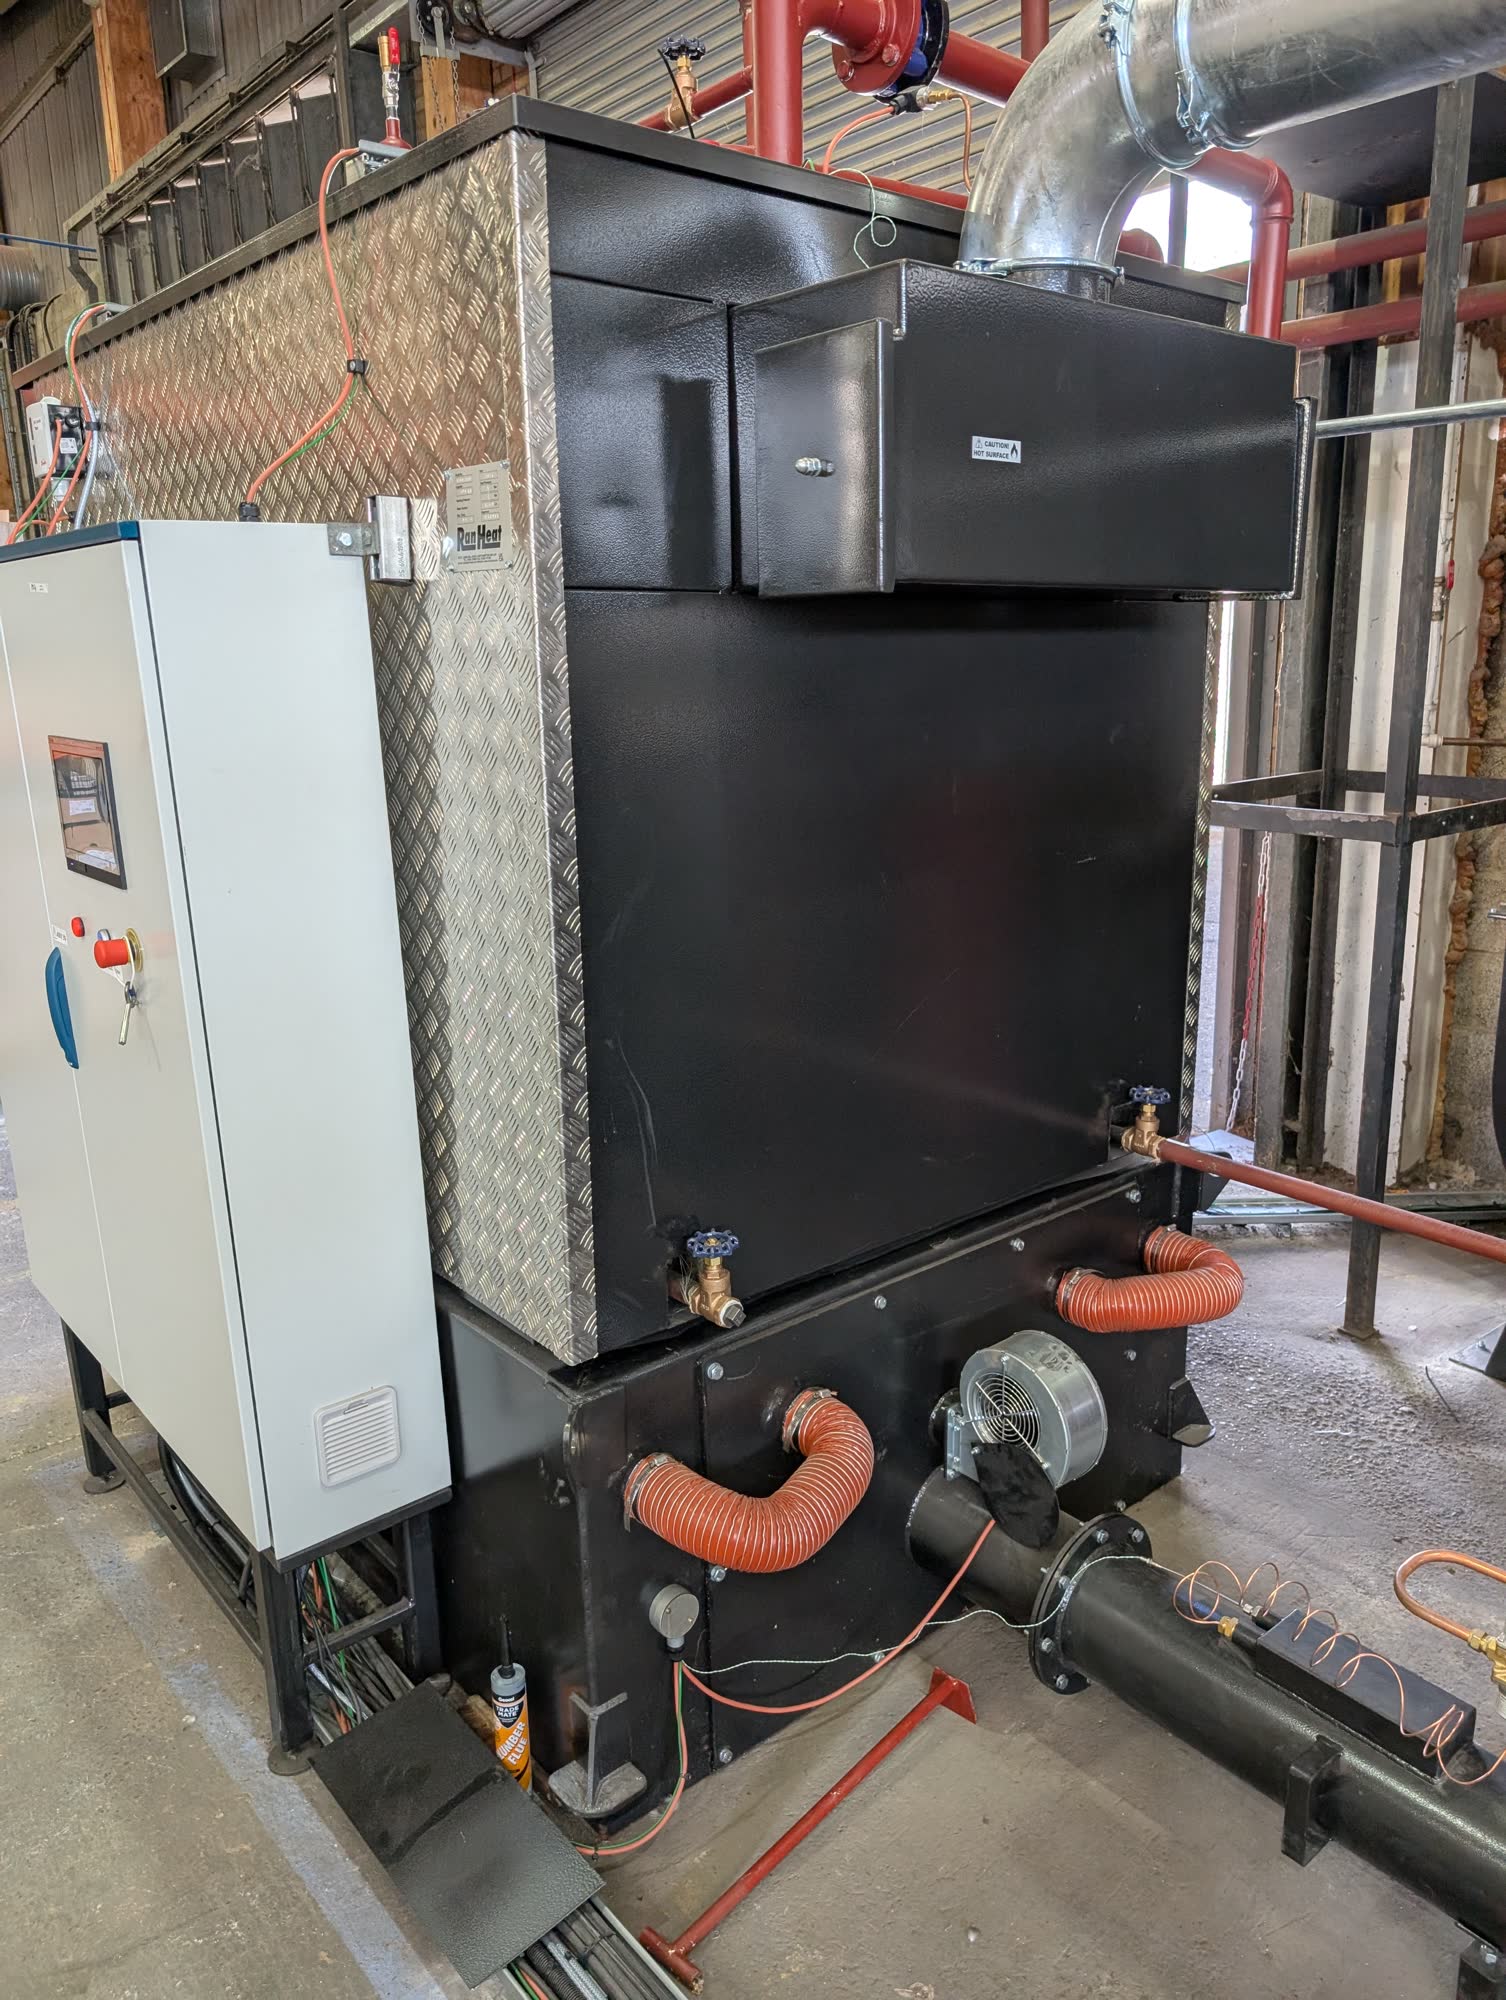
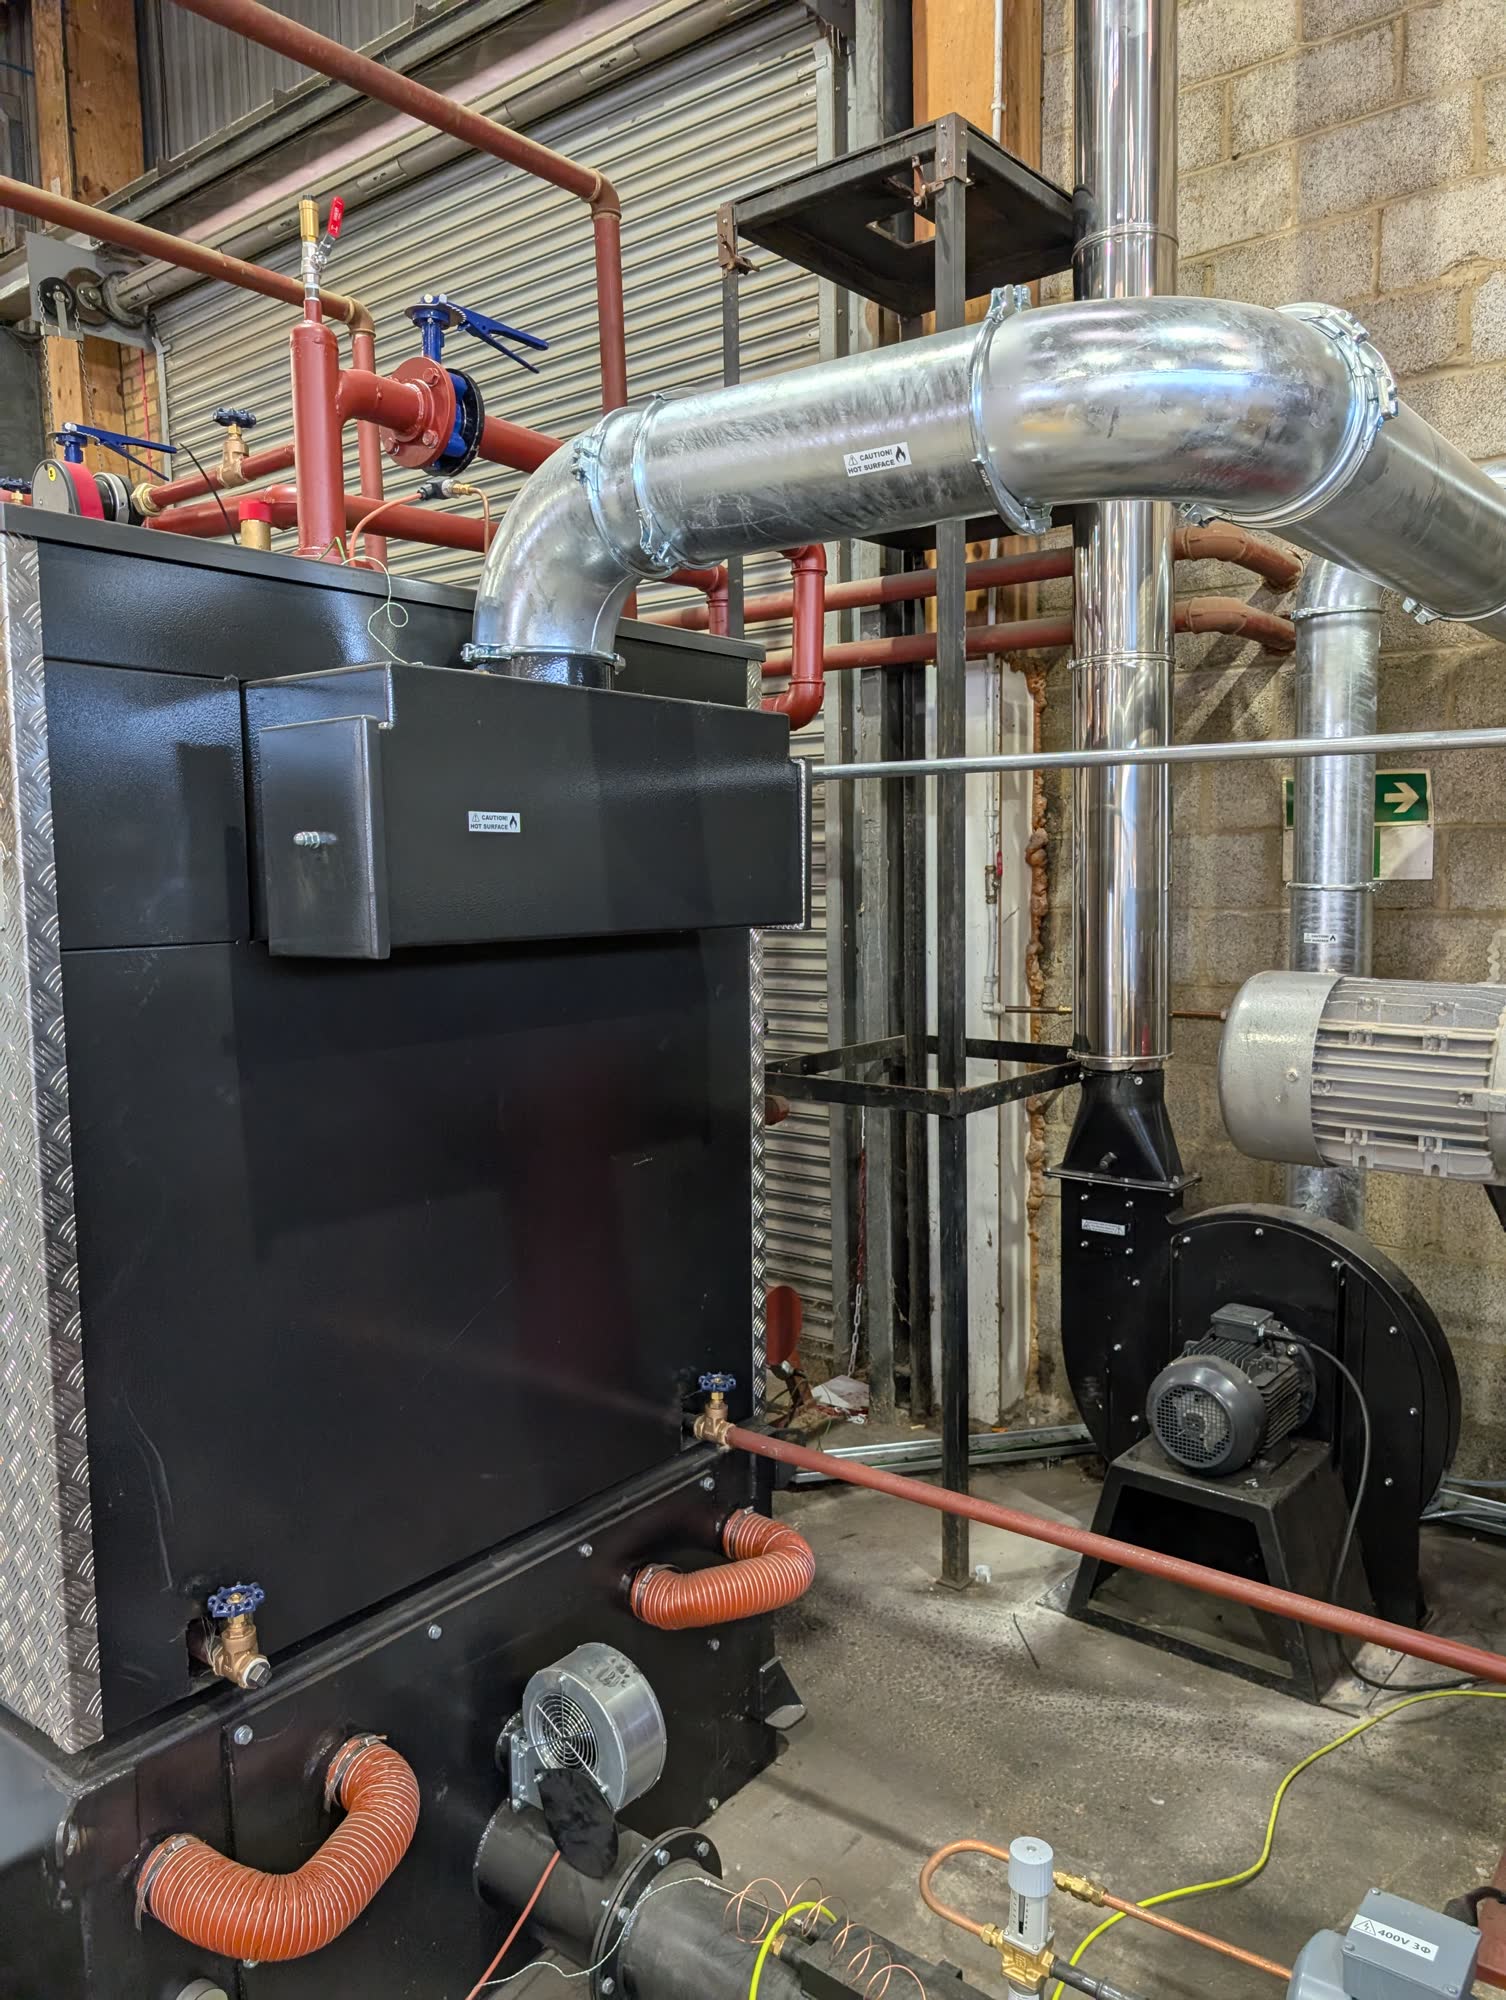
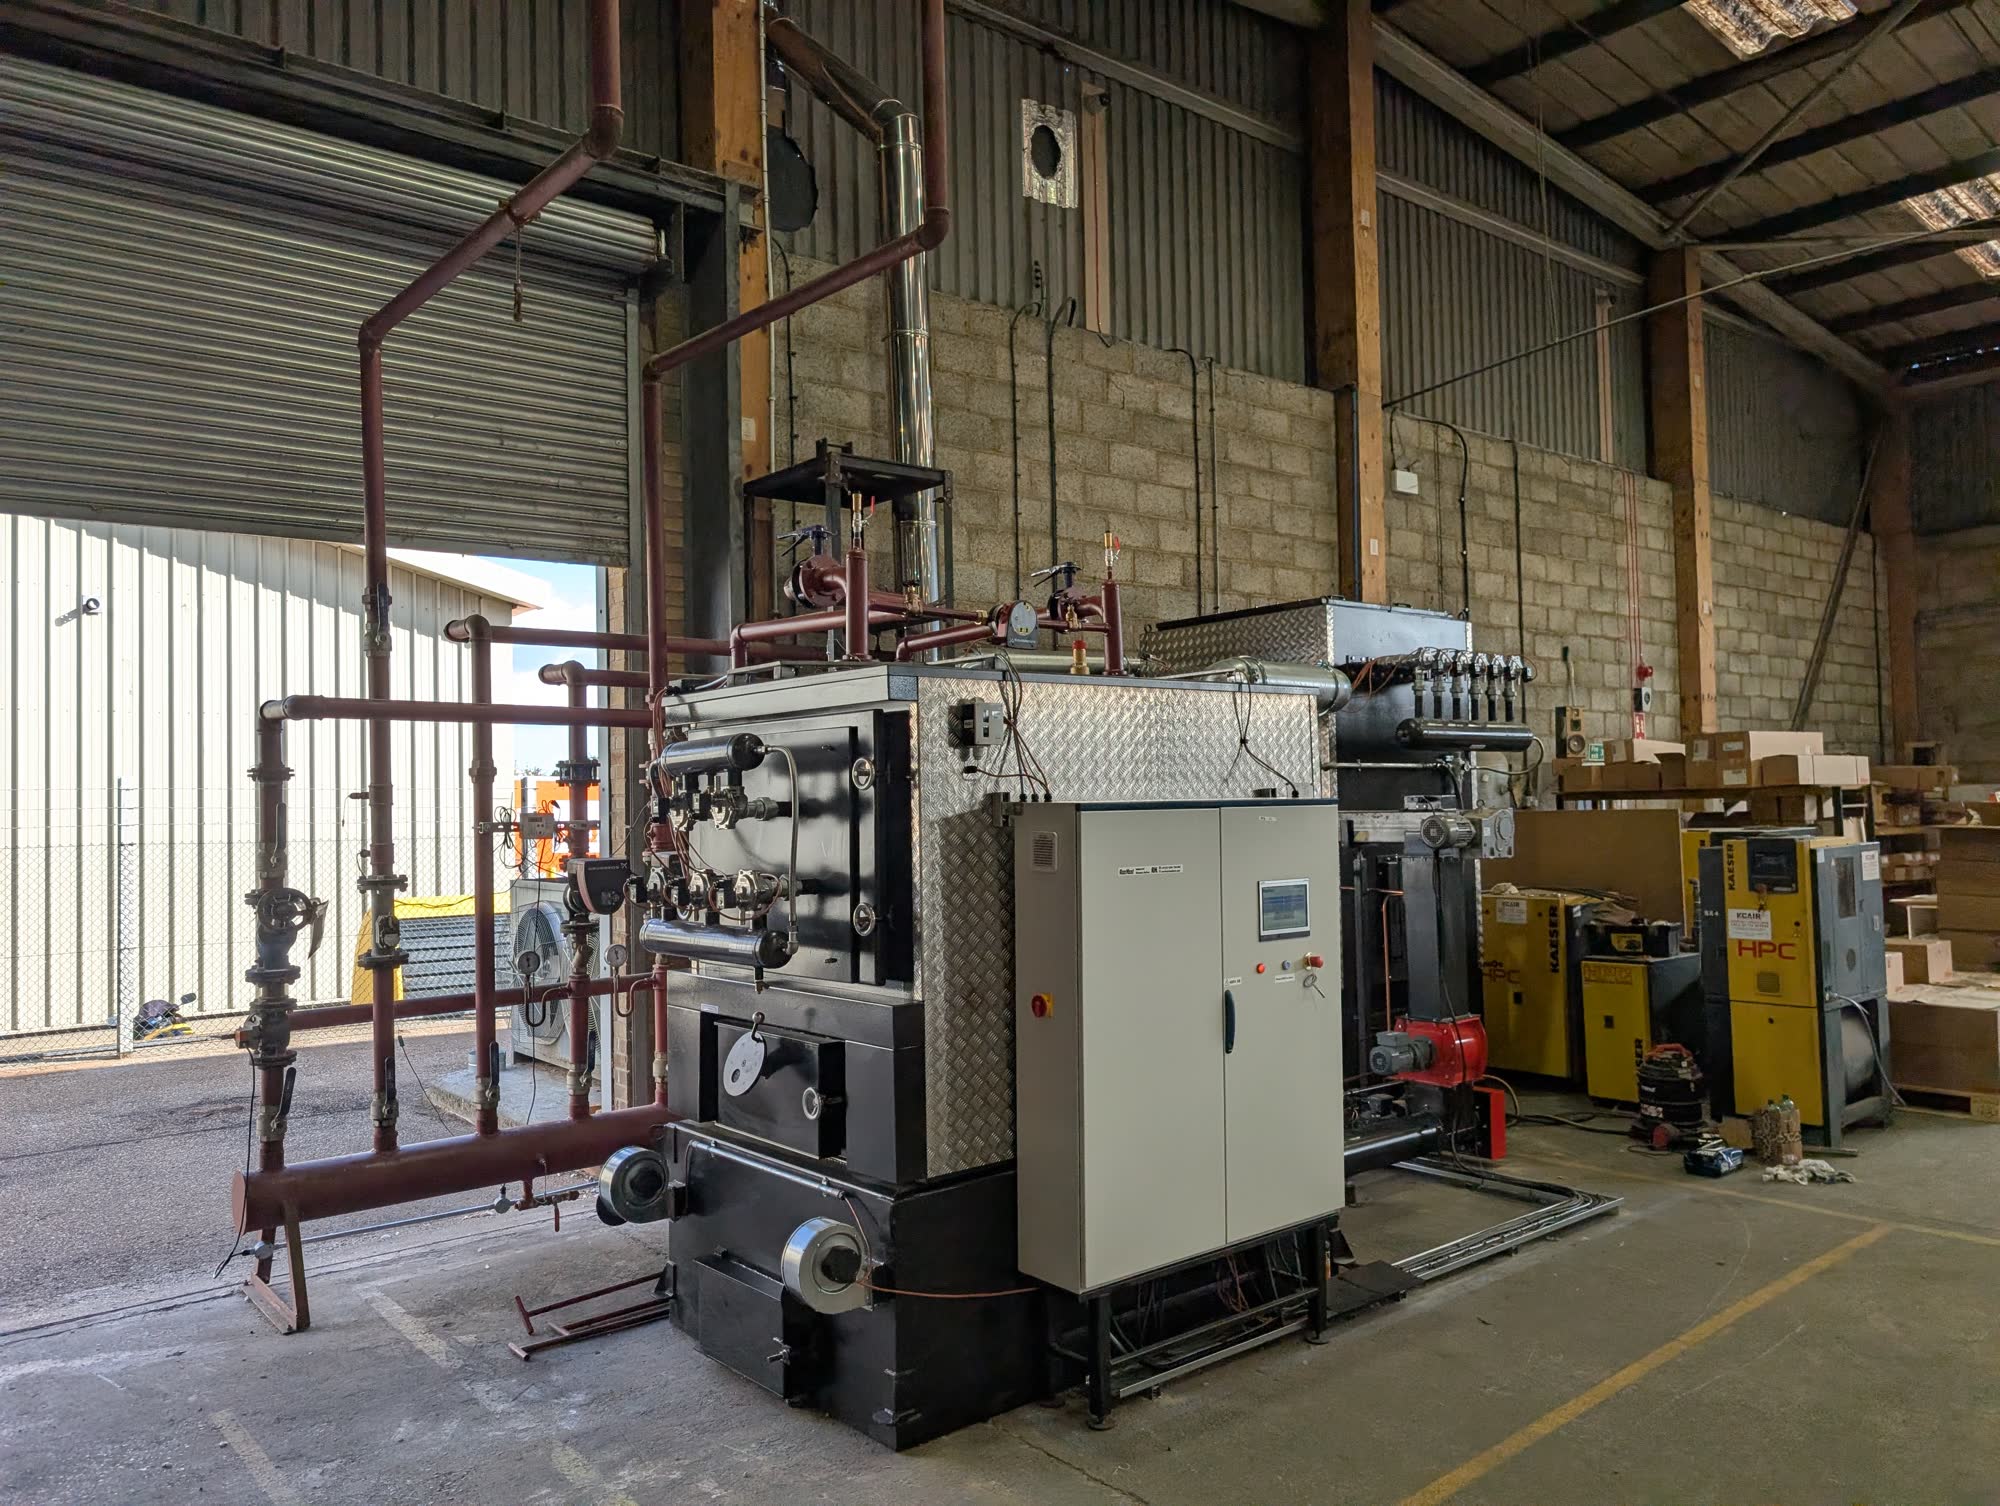
We then installed a Ranheat MSU300 with a ceramic filter, built in our Northampton factory and designed to fit with the existing plant at Kitchen Generator.
Accessible Floor-Level Layout
Crucially we were also able to reposition the ID fan at ground level, making it easily accessible. This simple choice made a huge difference for the Kitchen Generator team. The new layout also adds automatic tube cleaning, a viewing hatch, and puts the factory heating under the same control panel.
Advanced Combustion & Air Quality Features
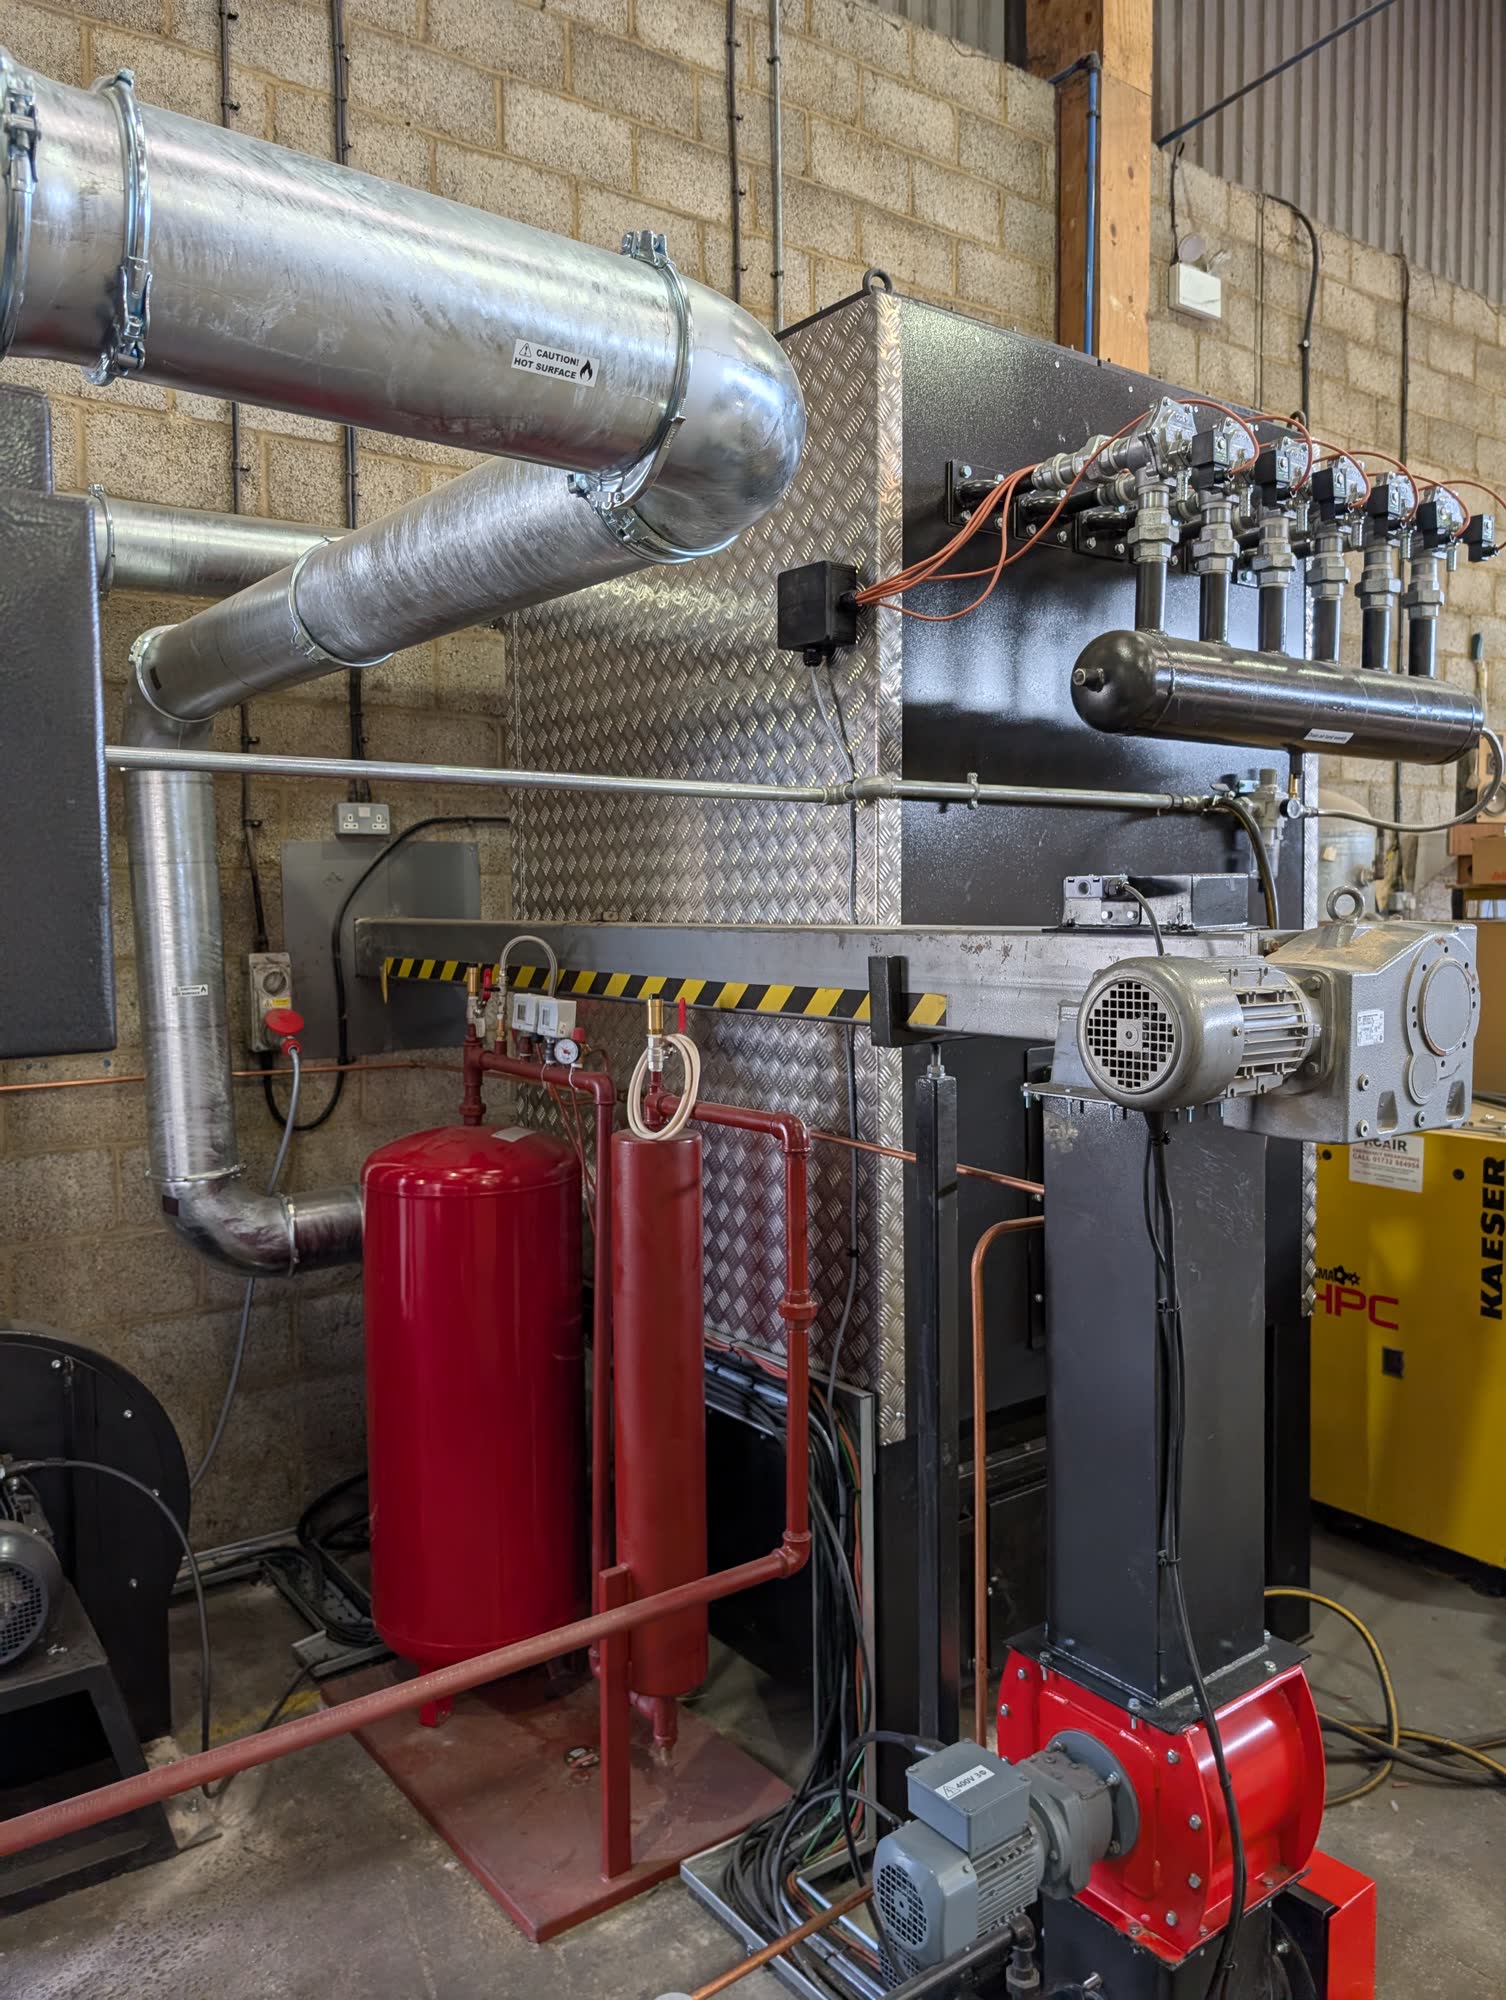
- Ceramic Filter Flue Gas Cleaning: Built with integrated pulse jet cleaning to ensure strict compliance with local emissions standards, even when burning high-resin fuels like MDF and chipboard.
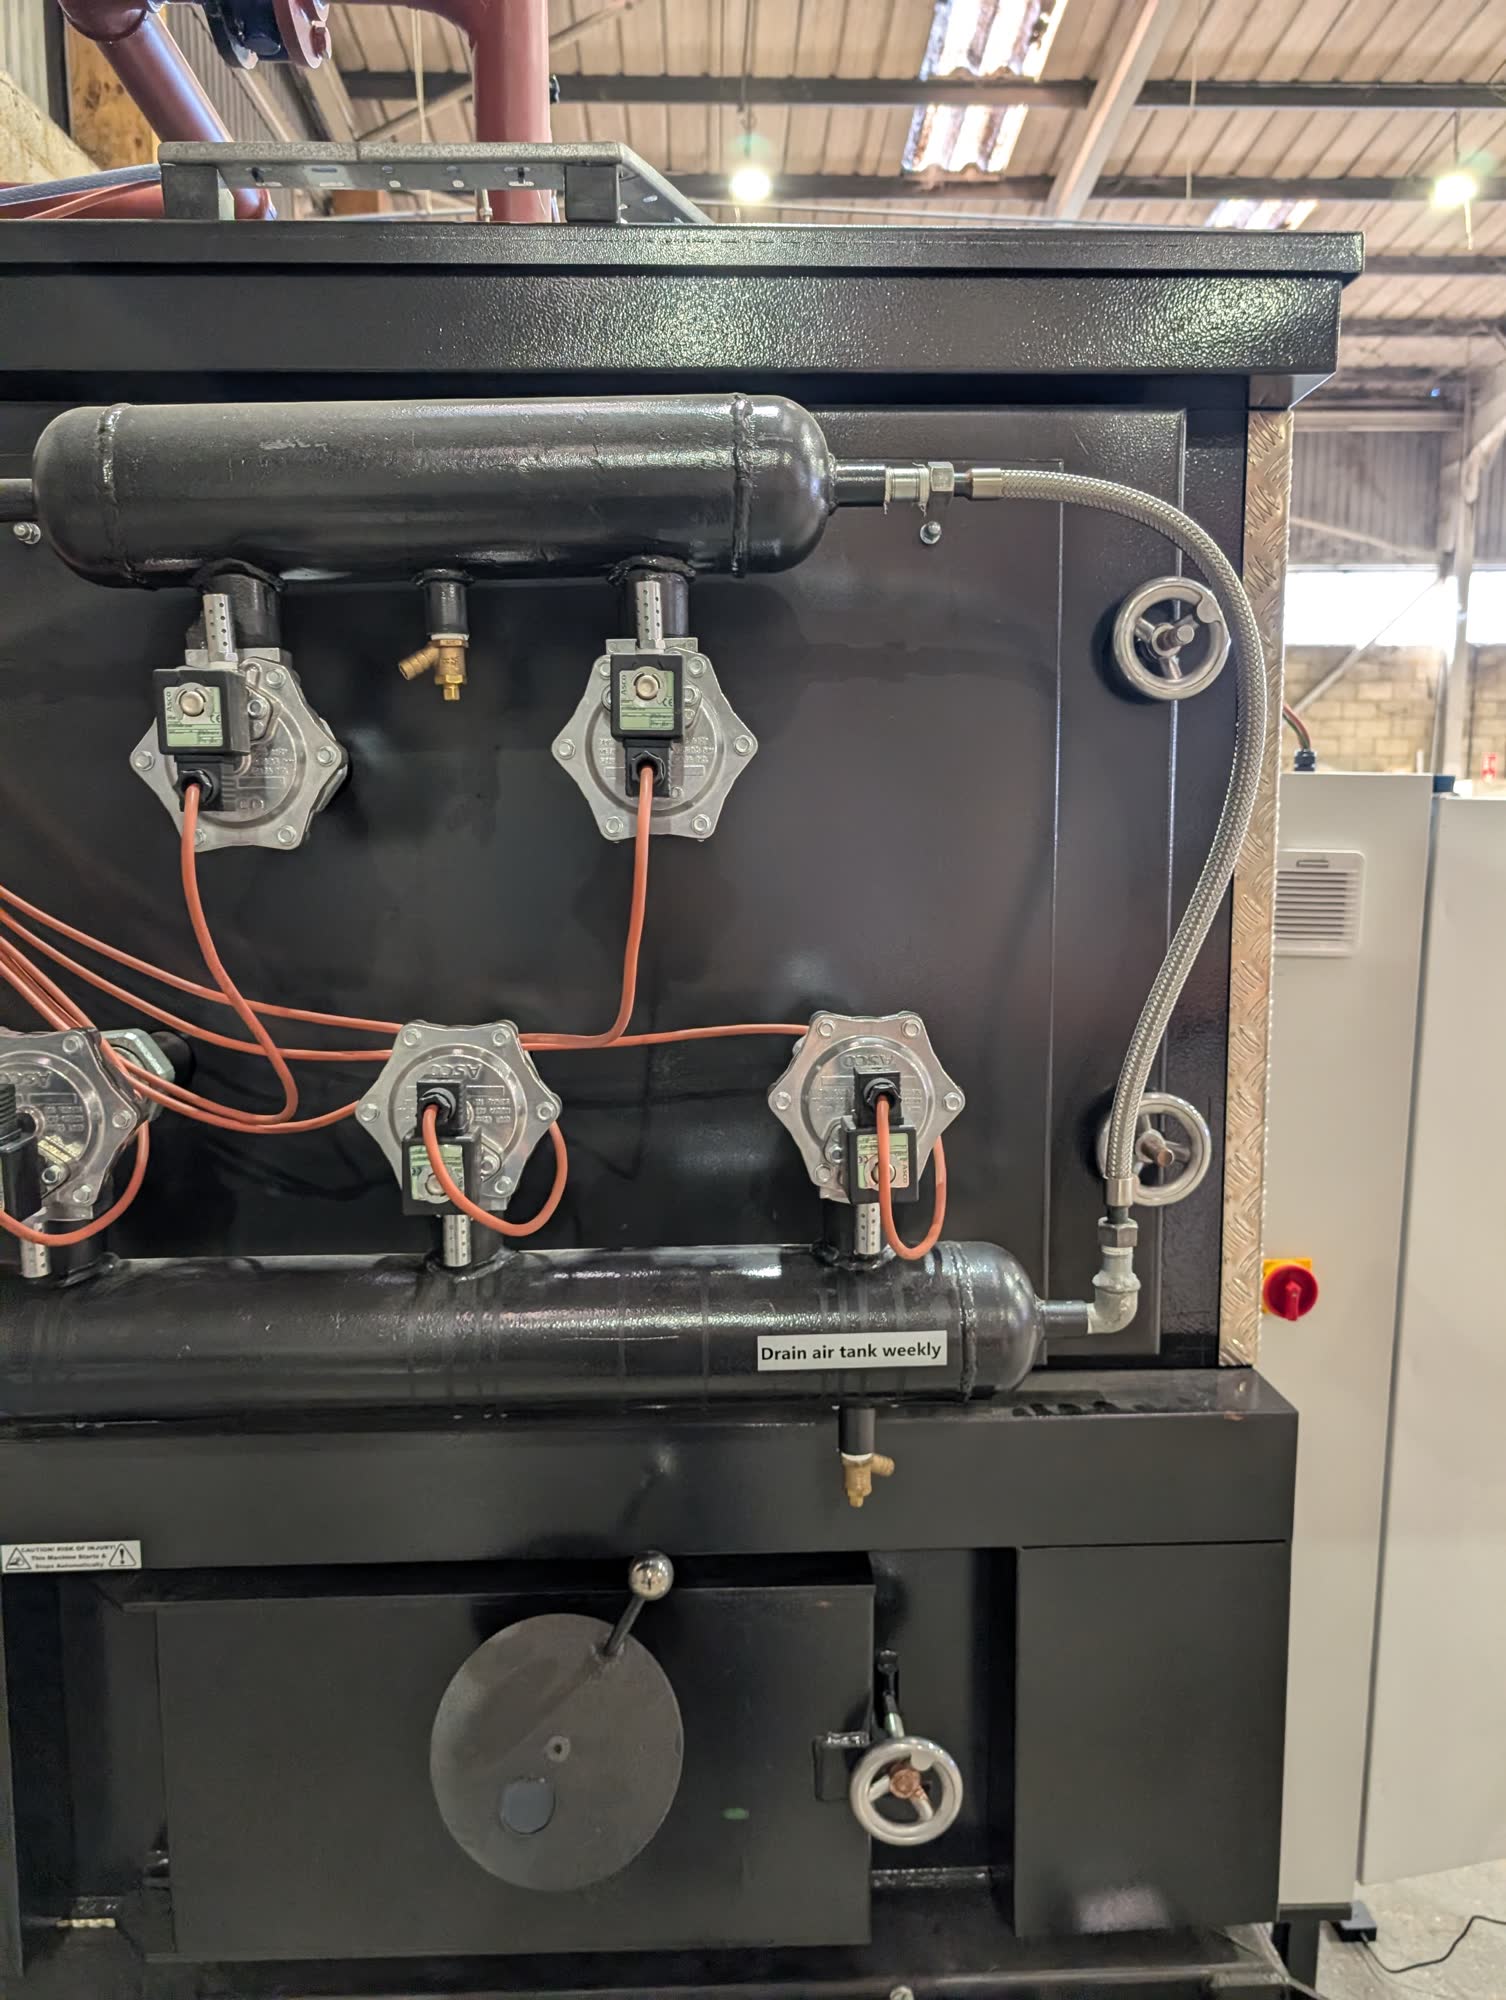
- Automatic Boiler Tube Cleaning: Large-throated solenoid valves mounted directly over the boiler tubes keep heat exchange surfaces clear of soot and fly ash automatically.
- Simplified Ash Management: Featuring a fixed retort stoker, bottom ash is cleared quickly through a simple access hatch without requiring an automatic de-ashing system.
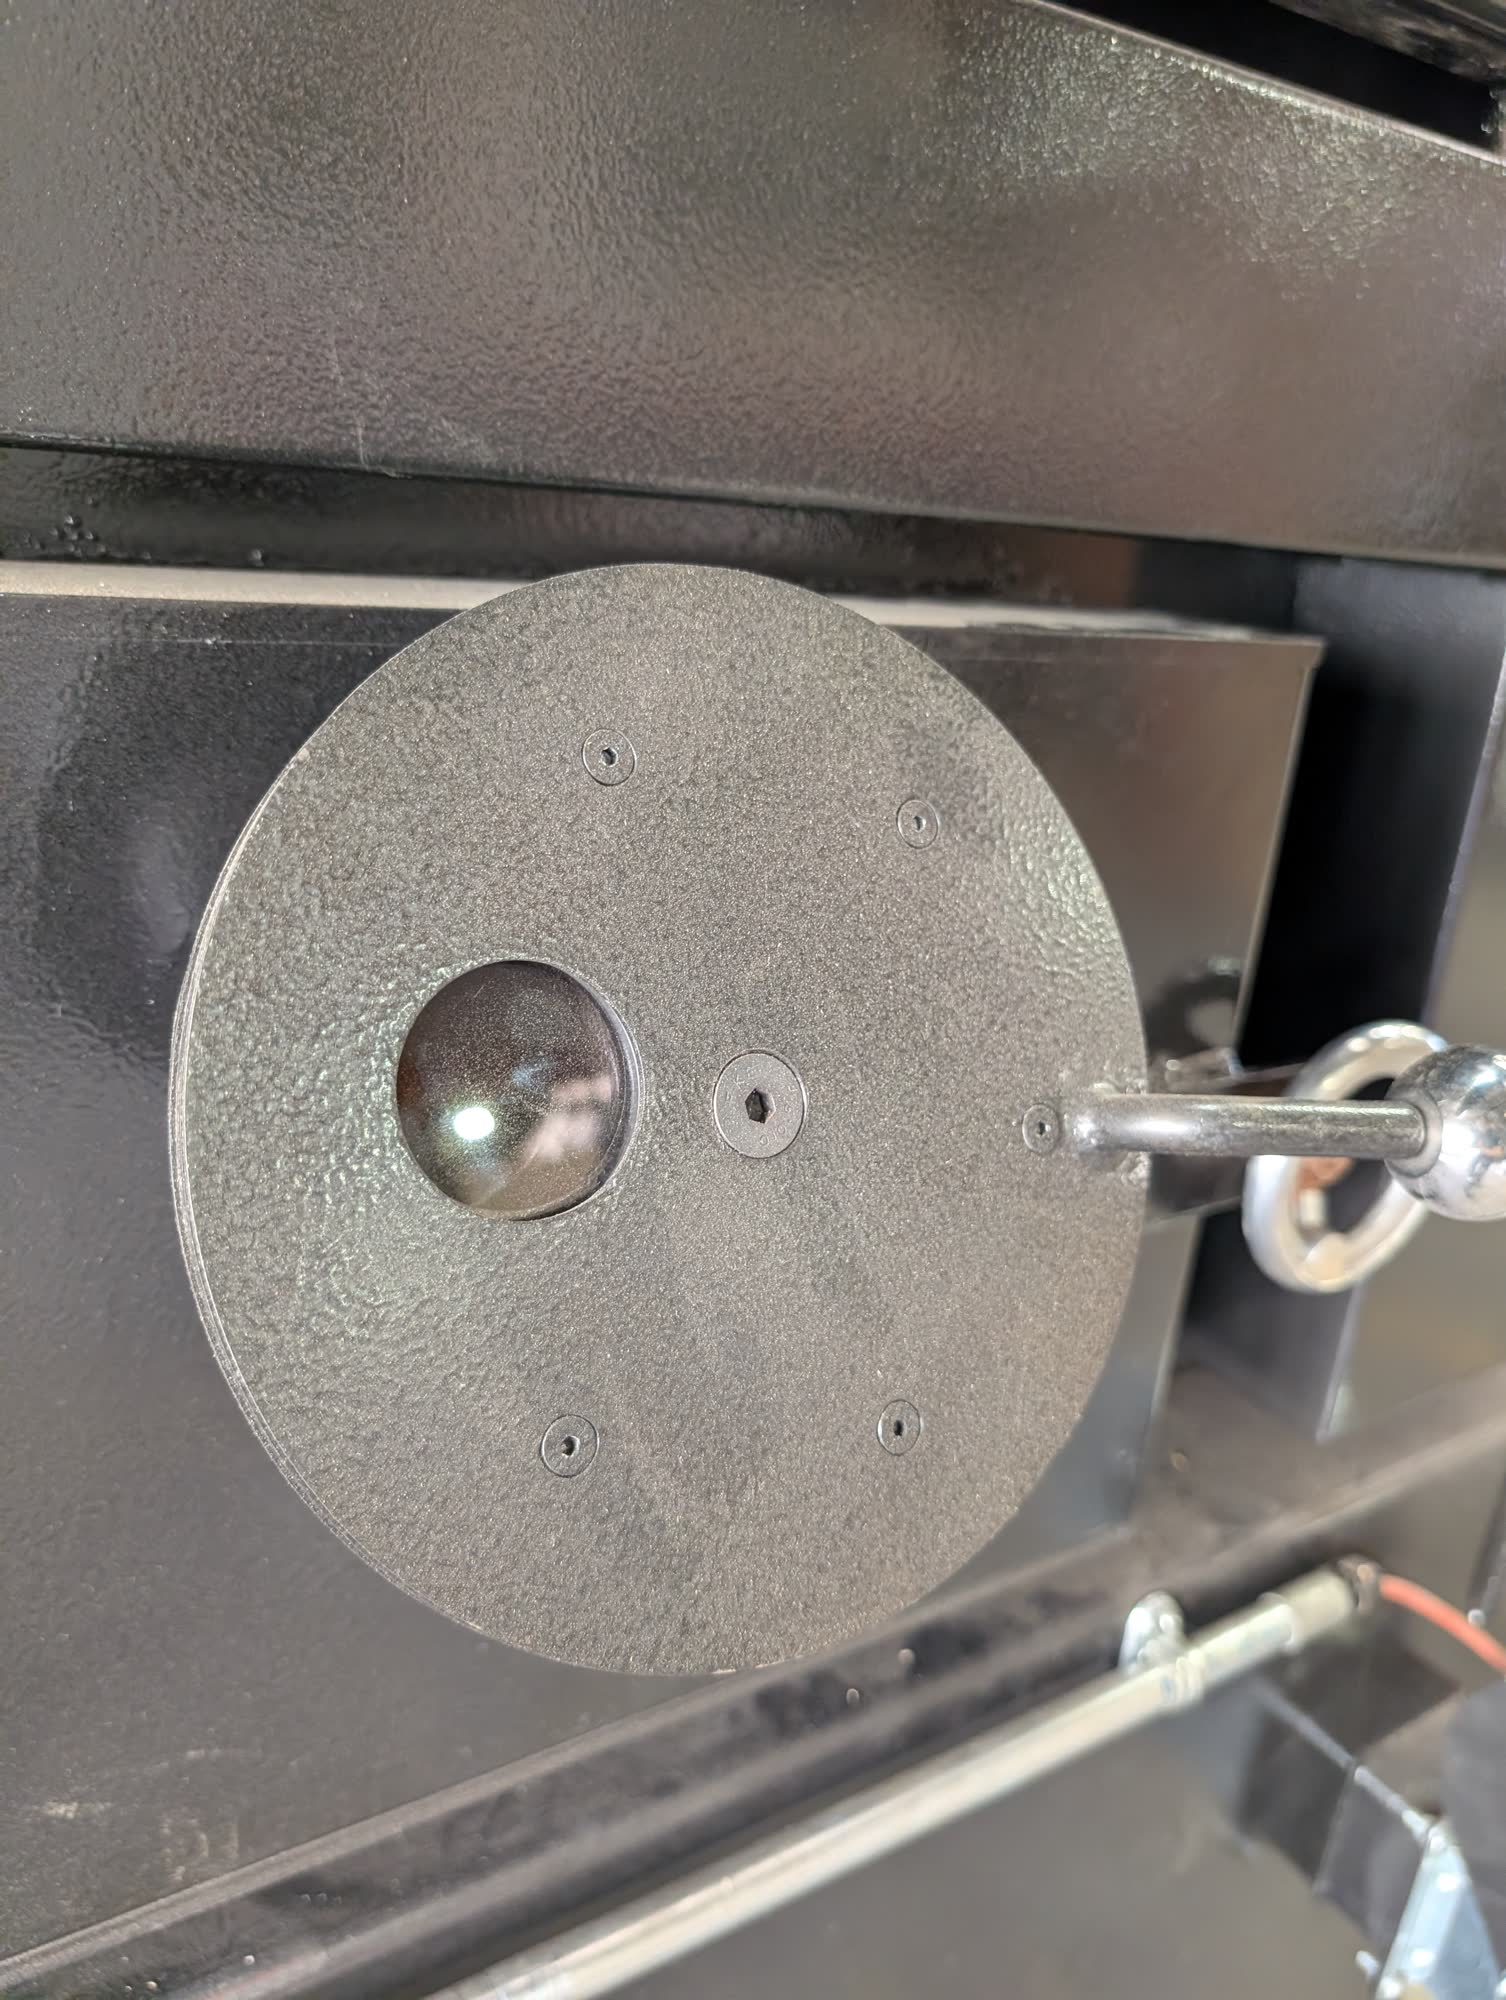
- Inspection Port: A Ranheat viewing hatch allows the team to make visual checks of combustion without opening fire doors.
Smart System Controls & RanheatIO Monitoring
While the engineering for the system is complex, it is hidden away and leaves just a simple control panel for the team to operate. This allows them to do only the three things they want: to heat the factory by conserving fuel or using as much as possible, or to dispose of as much waste as possible.
Four members of the Kitchen Generator team were trained to use the system, and the whole thing is connected to our remote monitoring system RanheatIO. This allows both the Kitchen Generator team and the Ranheat team to keep an eye on the performance of the whole system, and solve any problems as fast as possible, minimising downtime and cost.
This is a newly installed system, so we are yet to gather data on savings and efficiency, but the team at Kitchen Generator have already reported greater ease of use and convenience, as well as complete peace of mind that their biomass boiler system will not need expensive maintenance any time soon. They are also very pleased with the new placement of the ID fan.
Could a Ranheat Biomass System Be Right for Your Business?
If you are unsatisfied with the current boiler and heating setup at your business site, biomass or otherwise, get in touch with the Ranheat team to learn how we could help.
You can also learn more about our systems on our Frequently Asked Questions page.